Welding - internal aft access?

https://www.gullco.com/ceramic-weld...MIiI_45frD9AIV_wytBh08_AJGEAAYASAAEgKsc_D_BwE

I have include a single website that may provide an option to require welding from one side. I did not see.
So the concept is to attach a ceramic backer bar that enables a high heat root pass from one side only and the ceramic will "hold the shape of the weld bead and permit a weld pool that is homogeneous. Most people in the industry are aware of
the straight ceramic backing bars but at Fabtech maybe 10 years ago there was a company that used smaller squares, say 1 inch by 1/2 squares affixed to a sticky tape so that the squares could follow a curve.
So with proper cleaning, sticking the ceramic tape/backer to the hull from the open hole, then inserting the preformed patch, you would be able to get sound welds from one side only.

Video to show the process
So you would need only a few smaller holes cut in the deck to affix the backing, remove it and paint the finished weld

Love this ceramic tape
Here's a link to an Australian supplier Might have to give this a go I feel but I still wonder how I'll paint the internal weld.
 
For repairs I would cut out the entire step area, including the sides and inner transom (I drew it on the picture). Why, because from what I can see you have more work to do than just the corner, and the flat area around the step is simplest to reach from the inside for painting after rewelding. Depending on how you plan to use the boat you can reshape the stern to your liking.

If you can reach that corner from inside for painting you can cut the deck only in that area. The mooring clamp probably has to come out and be rewelded anyway, you don't know how far the rust goes under the paint.

If I were to cut the area you suggested, would I not still be left with the problem of painting the internal welded area after I weld that area back up ? I'll ahve a much better look this weekend once I'm back aboard.
 
She's a Van De Stadt HJB 41
upload_2021-12-2_22-10-48.png
 
If you have to remove the paint from the inside of the hull an option is to use a dry ice blast. Basically a machine grinds up frozen C02 and air blasts it. The advantage is that there is no abrasive to deal with, ie sand, walnut shells etc.
The only thing that you have left is the rust and paint. It can be used outside as well and in some marinas where they do not allow sandblasting, they often allow the dry ice method
There is a company called Cold Jet in Sydney, and probably others, mobile unit.
Dry ice blasting is extremely hazardous in a confined space. As the ice melts it floods the compartment with CO2 which will suffocate anyone in the area. You need to have air supply to a mask and preferably a gas monitor too.
 
If I were to cut the area you suggested, would I not still be left with the problem of painting the internal welded area after I weld that area back up ? I'll ahve a much better look this weekend once I'm back aboard.

Re the General Arrangement drawing posted above, it looks like you have a water-tight bulkhead on the forward side of the steering gear compartment?
I presume that there is an access hatch to get to the steering gear - it looks rather tight, but if you can weld it from the outside as per Barry's suggestion, would it not be possible to get inside through the hatch to paint the weld areas?

Edit - I just had another look at the photos on the first page, including the photo of the rudder stock and quadrant, and there does not appear to be a bulkhead as shown in the drawing. If you could get access to take the photo, you should have enough access for painting?
 
Last edited:
Dry ice blasting is extremely hazardous in a confined space. As the ice melts it floods the compartment with CO2 which will suffocate anyone in the area. You need to have air supply to a mask and preferably a gas monitor too.

A professional company would more than likely know this, wouldn't you think?
 
Love this ceramic tape
Here's a link to an Australian supplier Might have to give this a go I feel but I still wonder how I'll paint the internal weld.
You still will have to provide some inspection holes to be able to push the tape into the back of the insert from the inside BUT they do not need to be as large as holes that would be required to do weld from the inside.
The ceramic option is just that, an option as you can produce one side welded Welding Bureau approved welds from one side. There are millions of miles of oil field pipe lines welded, x-rayed etc from one side.
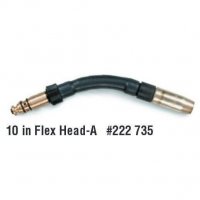
Not sure what welding head that you have on the Mig, but if it is a Spoolamatic or equivalent, you can purchase for about $100 a flexible transition piece between the gun and the nozzle to permit confine space welding
 
a Spoolamatic , a flexible transition piece between the gun and the nozzle to permit confine space welding
This sounds like the go I feel. something on a 90degree angle perhaps to get into confined spaces. I'll also have to push clean air through the space yes ? I'll take more pix tomorrow and post them here once I get back to the vessel. ( I just purchased her so have do a proper handover from the previous owner ) He might be able to show me the best interanl entry point as well.
 
A professional company would more than likely know this, wouldn't you think?
One would think. However, we see enough deaths in the industry that merits the comment.
 
This sounds like the go I feel. something on a 90degree angle perhaps to get into confined spaces. I'll also have to push clean air through the space yes ? I'll take more pix tomorrow and post them here once I get back to the vessel. ( I just purchased her so have do a proper handover from the previous owner ) He might be able to show me the best interanl entry point as well.

A flex nozzle permits just about any angle or a cobra (or equivalent push pull) gun

OR

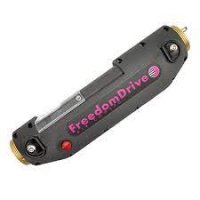
FreedomDrive™ | ABICOR BINZEL https://www.binzel-abicor.com/US/eng/products/manual/push-pull-torches/welding-torch-freedom-drive/?utm_term=wire%20feeder&utm_campaign=FreedomDrive+-+Q4+2021&utm_source=adwords&utm_medium=ppc&hsa_tgt=kwd-21499366&hsa_grp=131987258569&hsa_src=g&hsa_net=adwords&hsa_mt=b&hsa_ver=3&hsa_ad=558122429937&hsa_acc=2913790878&hsa_kw=wire%20feeder&hsa_cam=15141206390&gclid=EAIaIQobChMI7rqc14zI9AIVrh-tBh386Q5xEAAYAyAAEgJADfD_BwE

Quite the link address the website provided above. But the company is www.binzel-abicor.com

As a normal push pull gun is very long, it mainly offers a smaller head/nozzle. This unit is installed 6 feet away from the head and uses a small mig head assembly and appears to be smallest for limited access welding. The advantages then are a lighter head assembly and in a large production shop, the economy of buying 5 or 10 pound rools/spools or wire that can be mounted on the main welder.
 

Attachments

  • flex nozzle.jpg
    flex nozzle.jpg
    17.9 KB · Views: 328
  • cobra.jpg
    cobra.jpg
    2.5 KB · Views: 331
  • freedom.jpg
    freedom.jpg
    4.4 KB · Views: 300
Last edited:
Yesterday I took a trip back to the vessel and finally found some access points . This makes things 100% easier . Having said this I notice the port side aft corner suffers the same corrosion issue & on that side there seems to be no internal access... guess ya can't win em all right
NOTE: It's been raining hard here for weeks (Sydney Australia ) you'd think Summer time here now & yet all we get the past few weeks is grey cloud and constant rain.
I wait... :(
 
Last edited:
Forum posts represent the experience, opinion, and view of individual users. Boat Design Net does not necessarily endorse nor share the view of each individual post.
When making any potentially dangerous or financial decision, always employ and consult appropriate professionals. Your circumstances or experience may be different.

  • Back
    Top