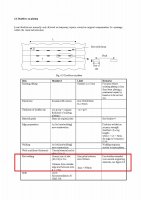
the layout of our boat link : https://youtu.be/myQcQaoQsLw
Our aluminum fishing boat pricipal dimensions
LOA 10.4M
LBP 8.66M
B(MLD) 2.7M
DEPTH(MLD) 0.85M
DRAFT(DLWL) 0.25M
aluminum : 5083alloy H321 made in Alcoa
all thickness of aluminum plates of our boat are 5mm.
A boat which have above dimensions is being built in our company and first ship.
We are very dificient..T_T
Today, we are getting into very large problem.
Originally we intended to single welding upperdeck to side shell plate.
But, Korea ship safety and technology Authority's inspector want us to double sides welding of upper deck.
but, we can't weld beneath upperdeck. as you see our dimensions, the depth is very low. so worker can't get into under deck. besides, In the single weldingng, the depth of penetration is enough for a strength aspect.
so we think that The double welding isn't needed and also we can't carry out double welding.
But, the inspector want us to double welding.
cf) There aren't any Law of welding less than 24meter in Korea.
and also, there are no shipbuilding with aluminum company for Fishing boat(less than 24meter.)
so, We can't find any case of aluminum boats in korea. help me..
How shall i do?
If u guyz have any information or photos that carry out single welding of upperdeck in aluminum boat, please send me as soon as possible.
email:wonmin@sdn-i.com
our all product lines stop now...